

Thread milling
Solid Carbide Thread Mills
Over 750 Carmex solid carbide thread mills for CNC machining centres, in 16 thread forms from Metric and UN to BSP, NPT, ACME and aerospace MJ and UNJ. Choose by thread form, by the type of tool the job needs, or by the material you are cutting. Order by 4.30pm for same-day dispatch.
Option 1
Shop by Thread Form
Start with the thread on the drawing. The thread form sets the flank angle and the pitch series, and each thread mill is ground for one form. Pipe threads, Whitworth, PG and the partial-profile tools cut internal and external threads with the same cutter.
Metric & Unified (60°)
 60°
Metric ISO
The standard metric thread, coarse and fine pitch. From M1 x 0.25 upwards.
View Metric thread mills60°UN (UNC, UNF, UNEF, UNS)
Unified inch threads for imperial-drawn parts, from 0-80 UNF upwards.
View UN thread mills60°MJ
Metric aerospace thread with a controlled root radius for fatigue life.
View MJ thread mills60°UNJ
The inch version of MJ, with a controlled root radius. Formerly MIL-S-8879.
View UNJ thread millsBritish 55° threads
55°BSP (G)
Parallel pipe thread for ports that seal on a washer or O-ring.
View BSP thread mills55° · 1:16BSPT (R, Rc)
Tapered pipe thread that seals on the thread itself.
View BSPT thread mills55°Whitworth (BSW, BSF)
Coarse and fine Whitworth for older British machinery and fixtures.
View Whitworth thread millsAmerican pipe threads (60°)
60° · 1:16NPT
US tapered pipe thread, sealed with tape or compound.
View NPT thread mills60° · 1:16NPTF
Dryseal taper that seals metal to metal, for hydraulics and fuel lines.
View NPTF thread mills60°NPS
Straight pipe thread for joints that do not seal on the thread.
View NPS thread mills60°NPSF
Dryseal straight internal thread that mates with an NPTF male.
View NPSF thread millsConduit & motion threads
80°PG (DIN 40430)
Steel conduit thread, still used on cable glands and electrical fittings.
View PG thread mills29°ACME
Inch trapezoidal thread for lead screws, jacks and vices.
View ACME thread mills30°Trapez (Tr)
The metric trapezoidal thread for lead screws and linear drives.
View Trapez thread millsPartial profile: one tool, several pitches
60°60° Partial Profile
Cuts the flanks only, so one tool covers a range of pitches. Internal and external.
View 60° partial profile thread mills55°55° Partial Profile
The same idea for 55° threads. One cutter, several pitches, internal and external.
View 55° partial profile thread millsOption 2
Shop by Tool Type
Once you know the thread, the job decides the tool: how deep the thread is, how small the hole is, how many parts you are making and whether your machine has through-spindle coolant. Each type covers every thread form it is made in.
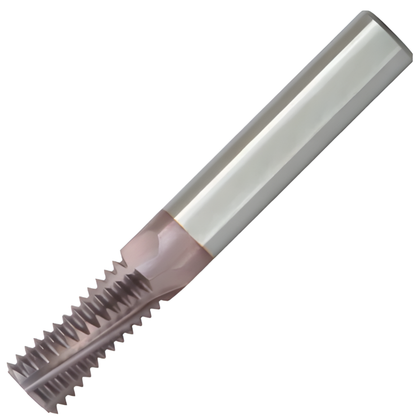
Full Profile Thread Mills
One 360° orbit cuts the whole thread length. The shortest cycle for production threads, with 3 to 8 flutes. Carmex MT, MTB, MTZ and FMT.
Shop full profile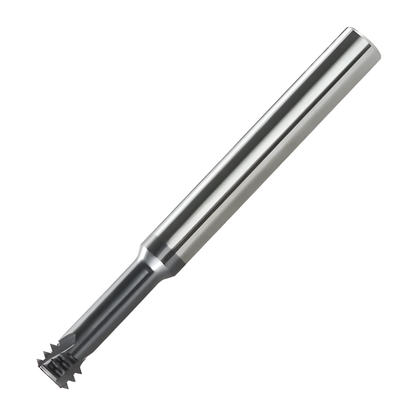
Mini Thread Mills
Low cutting force for small threads, deep threads and thin walls. Threads from M1 x 0.25 and 0-80 UNF. Carmex MTS, MTSB and MTI.
Shop mini thread mills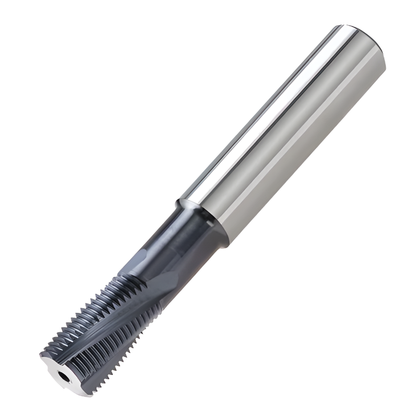
Long Reach Thread Mills
A short cutting edge on a relieved neck for medium and large threads deep in a part or at the bottom of a pocket. Carmex MTQ.
Shop long reach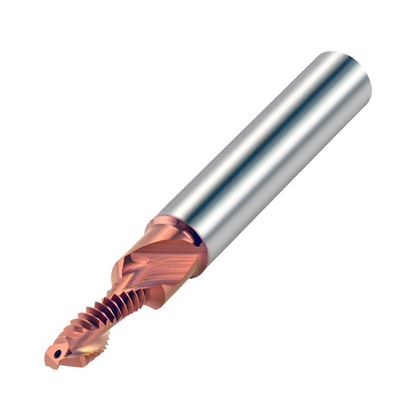
Drill Thread Mills
One tool makes the hole, the chamfer and the thread, so there is no pilot drill and no tool change. Carmex MTD, DMT and DMTH.
Shop drill thread mills
External Thread Mills
Metric, UN, MJ and UNJ tools made for external threads, with spiral flutes for a clean finish. Carmex MT.
Shop external thread mills
Through-Coolant Thread Mills
Coolant through the tool flushes chips out of blind holes and cools the edge. Needs through-spindle coolant. MTB, MTZ, MTSB and more.
Shop through-coolantThreads too big for solid carbide? See our indexable thread mills, which take replaceable inserts.
Option 3
Shop by What You Are Cutting
The ISO material groups, in the colours the standard uses. The grade and edge matter as much as the thread form: a coated tool that runs all day in steel will clog in aluminium, and a general grade will not survive hardened steel.
Steel, Stainless & Cast Iron
Most Carmex thread mills use MT7, a sub-micron carbide with a TiAlN multi-layer coating, for steel, stainless and cast iron in the soft and pre-hardened state.
Shop all thread mills
Aluminium & Non-Ferrous
Aluminium sticks to a coated edge and packs the flutes. Carmex AMT tools have a polished uncoated edge and a coolant bore; AMT-C adds a cutting chamfer.
Shop aluminium thread mills
Hardened Steel & Superalloys
MTSH and MTH cut steels up to 62 HRC, and MTH also takes titanium and Inconel. FSH, in the MT3 grade with up to 7 flutes, goes to 65 HRC. DMTH drills and threads hard parts in one.
Shop hardened thread millsThe Right Thread Mill, in Seconds
Answer three questions and get the exact Carmex thread mill and cutting data for your job, from stock in Kent.
Launch the Wizard
Full Profile, Mini or Partial Profile?
All thread mills cut by helical interpolation: the tool runs round the hole while the Z axis moves one pitch per turn. What differs is how much of the thread each tool cuts in one go.
| Type | How it cuts | Pitches per tool | Best for | Carmex series |
|---|---|---|---|---|
| Full profile | Several rows of teeth. One 360° helical orbit cuts the whole thread length the edge covers. | One | Production runs and short cycle times on standard sizes | MT, MTB, MTZ, FMT |
| Mini (short profile) | A few teeth on a slim neck. Follows a helical path along the full depth, one pitch per turn. | One | Small threads, deep threads, thin walls and set-ups where cutting force must stay low | MTS, MTSB, MTI, MTQ |
| Partial profile | Cuts the thread flanks only. The diameter and depth come from the program. | A range, in one flank angle | Small batches, odd pitches and shops that want fewer tools on the shelf | MTI 60° and 55° partial profile |
| Drill thread mill | Drills the hole, chamfers the edge, then mills the thread. | One | High-volume parts where a tool change costs more than the tool | MTD, DMT, DMTH |
Thread Form Reference
The flank angle, taper and standard for every thread form we stock thread mills in, and whether one Carmex tool cuts both the internal and the external thread.
| Thread form | Flank angle | Taper | Standard | Where you find it | Carmex tools cut |
|---|---|---|---|---|---|
| Metric ISO (M) | 60° | Parallel | ISO 68-1, ISO 261 | General engineering worldwide | Internal; separate external tools |
| UN (UNC, UNF, UNEF, UNS) | 60° | Parallel | ASME B1.1 | US and imperial-drawn parts | Internal; separate external tools |
| MJ | 60°, rounded root | Parallel | ISO 5855 | Metric aerospace fasteners | Internal; separate external tools |
| UNJ | 60°, rounded root | Parallel | ASME B1.15 | Inch aerospace fasteners | Internal; separate external tools |
| BSP (G) | 55° | Parallel | ISO 228-1 | Hydraulic and pneumatic ports sealed by washer or O-ring | Internal and external, same tool |
| BSPT (R, Rc) | 55° | 1:16 | ISO 7-1 (BS 21) | Pipe joints that seal on the thread | Internal and external, same tool |
| Whitworth (BSW, BSF) | 55° | Parallel | BS 84 | Older British machinery and fixtures | Internal and external, same tool |
| NPT | 60° | 1:16 | ASME B1.20.1 | US pipe fittings, sealed with tape or compound | Internal and external, same tool |
| NPTF | 60° | 1:16 | ASME B1.20.3 | Dryseal metal-to-metal joints | Internal and external, same tool |
| NPS | 60° | Parallel | ASME B1.20.1 | Straight pipe joints that do not seal on the thread | Internal and external, same tool |
| NPSF | 60° | Parallel | ASME B1.20.3 | Dryseal straight internal ports | Internal and external, same tool |
| PG | 80° | Parallel | DIN 40430 | Cable glands and electrical conduit | Internal and external, same tool |
| ACME | 29° | Parallel | ASME B1.5 | Inch lead screws, jacks and vices | Internal |
| Trapez (Tr) | 30° | Parallel | ISO 2904, DIN 103 | Metric lead screws and linear drives | Internal |
The 60° and 55° partial-profile tools cut the flanks of any thread with that angle, internal or external, across a range of pitches.
Four Checks Before You Order
Get these right and the thread mill will fit the hole, reach the depth and cut the thread on the drawing.
- 1
Thread Form and Pitch
Take both from the drawing: M10 x 1.5, 1/4-20 UNC, G 1/2 and so on. A thread mill is ground for one pitch, so the pitch must match exactly. A partial-profile tool covers several pitches in one flank angle.
- 2
Hole Size and Tool Diameter
The tool's cutting diameter has to pass into the drilled hole with room to orbit. The specification on each product lists the smallest thread it will cut. Drill the same size you would for a tap.
- 3
Thread Depth and Reach
Check the cutting length and reach against the thread depth. Full-profile tools cut up to their cutting length in one orbit; for deeper threads use a mini or long reach tool.
- 4
Material and Coolant
Pick the grade for the material, and a coolant-bore or through-flute tool if your machine has through-spindle coolant. It matters most in deep blind holes, where chips have nowhere to go.
Thread Mill Questions
The questions we are asked most about choosing and running solid carbide thread mills.
Is thread milling better than tapping?
Tapping is quicker for standard sizes in free-cutting materials. Thread milling wins when a broken tap would scrap an expensive part, in tough materials such as stainless, titanium and hardened steel, in blind holes where the thread has to run close to the bottom, and on large or unusual sizes. One thread mill cuts any diameter above its own size at the same pitch, and you adjust the thread fit with a tool offset instead of buying another tap. Our thread milling guide covers the comparison in full.
Can one thread mill cut different thread sizes?
Yes, as long as the thread form and pitch are the same. A full-profile tool ground for 1.5 mm pitch Metric will cut M12 x 1.5, M16 x 1.5, M20 x 1.5 and any larger 1.5 mm pitch thread, because the diameter comes from the circular path in the program. It will not cut M12 x 1.75, which needs a 1.75 mm pitch tool. The smallest thread it can cut is set by its cutting diameter, which has to fit in the drilled hole. Partial-profile tools go further and cover a range of pitches.
Can the same thread mill cut internal and external threads?
It depends on the thread form. Carmex tools for Metric ISO, UN, MJ and UNJ are made for internal threads, with separate MT tools for external threads, because the root of a nut thread and a bolt thread is a different shape. Pipe-thread tools (BSP, BSPT, NPT, NPTF, NPS and NPSF), Whitworth, PG and the 60° and 55° partial-profile tools cut internal and external threads with the same cutter. Each product page says which it is.
Full profile, mini or partial profile: which do I need?
Full-profile tools have several rows of teeth and cut the whole thread length in one 360° orbit, so they give the shortest cycle for production threads. Mini tools have a short cutting profile on a slim neck and follow a helical path along the full depth, which keeps cutting force low for small threads, deep threads and thin walls. Partial-profile tools cut only the flanks, so one tool covers several pitches with the same flank angle. Drill thread mills also make the hole.
How do I program a thread mill?
With helical interpolation: the tool moves round a circle with G02 or G03 while Z moves one pitch per revolution. For a right-hand internal thread, climb milling means starting at the bottom and working up with G03; a left-hand thread reverses the direction. Use cutter radius compensation so you can adjust the fit with an offset, and allow for the feed at the tool centre being lower than at the cutting edge. The Carmex Tool Wizard gives the tool, cutting data and CNC program for your thread.
Do I need a different thread mill for left-hand threads?
Not for most Carmex thread mills. The hand of the thread comes from the direction of the helical move, not the tool, so the same cutter makes right-hand and left-hand threads with a reversed program. Some series are made to run with the spindle in reverse (M04), and where that applies it is shown in the specification on the product page. Check it before you write the program.
Can thread mills cut hardened steel?
Yes, with the right grade. Most Carmex thread mills use MT7, a sub-micron carbide with a TiAlN multi-layer coating, for general work in steel, stainless and cast iron up to about 45 HRC. For harder work, MTSH and MTH are made for steels up to 62 HRC, and MTH also cuts titanium and nickel alloys such as Inconel. FSH uses the MT3 grade with up to 7 flutes for up to 65 HRC, and DMTH drills and threads hardened parts in one tool.
What size hole do I drill before thread milling?
The same tap-drill size you would use for tapping, which gives the thread's minor diameter: 8.5 mm for M10 x 1.5 and 10.2 mm for M12 x 1.75, for example. The thread mill's cutting diameter must be smaller than that hole, and its cutting length or reach must cover the thread depth. Drill thread mills (MTD, DMT and DMTH) make the hole themselves, so they need no pre-drilled hole.
Not Sure Which Thread Mill?
Answer three questions in the Carmex Tool Wizard for the exact tool and cutting data, or call our technical team with your drawing. Everything on this page is held in UK stock.
