

Carbide Burrs by Application
155 Vortex tungsten carbide burrs in 13 shapes, Types A to N. Pick by the shape you already run, or work down from the job you are trying to do.
Shop by burr shape
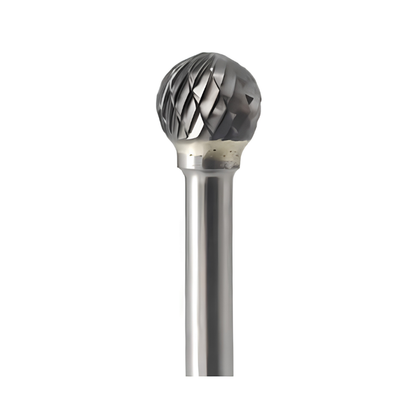
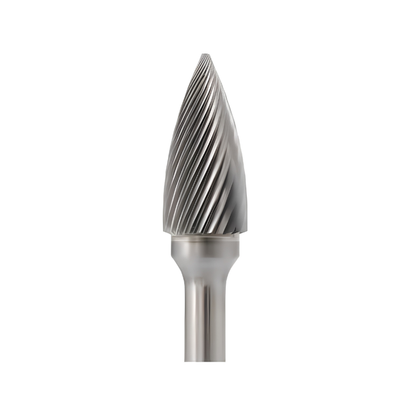
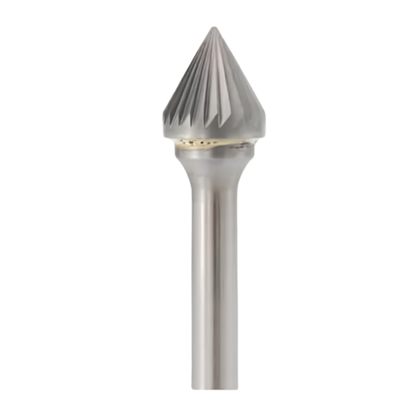
All thirteen shapes in the Vortex range, in order. There is no Type I — it is skipped in the standard series so it cannot be misread as a 1. Each shape is stocked in the cut styles shown on its card.
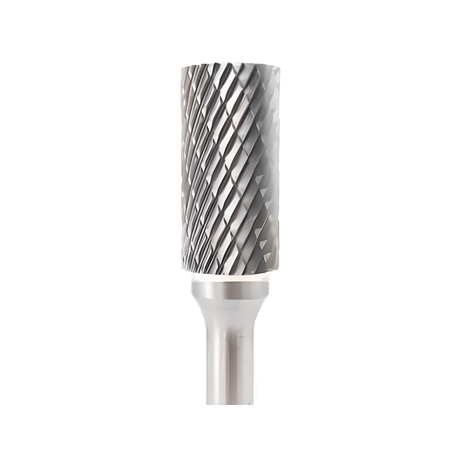
Type A
Flank-cutting only. Opens out and trues a hole or a slot wall without touching the floor of a pocket.
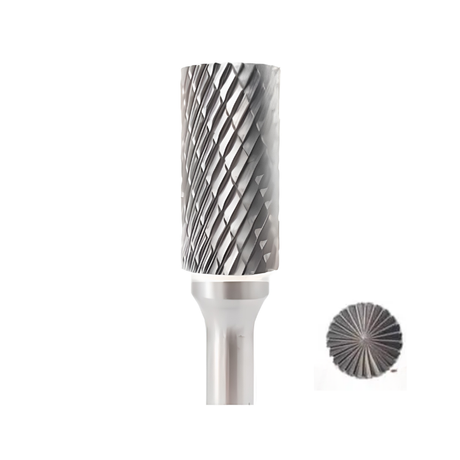
Type B
Teeth on the end as well as the flank, so it plunges in and then traverses. The general-purpose cylinder.
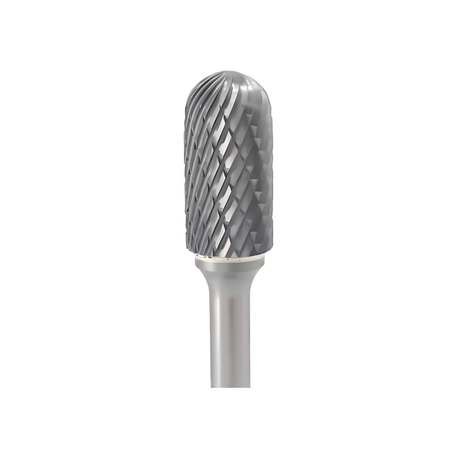
Type C
A cylinder with a radiused nose. Takes a radius into a straight wall in one setup, without a facet at the join.
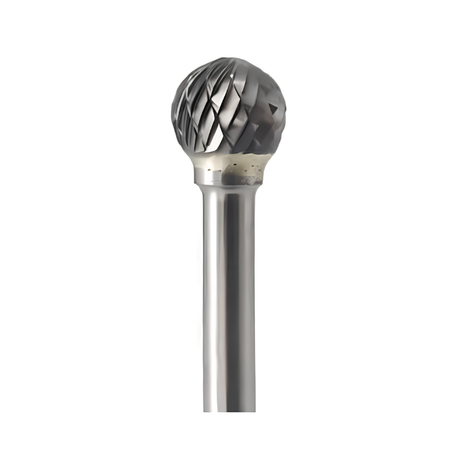
Type D
A plain ball. Drops into a concave radius and cuts in any direction. The most-used shape for blending work.
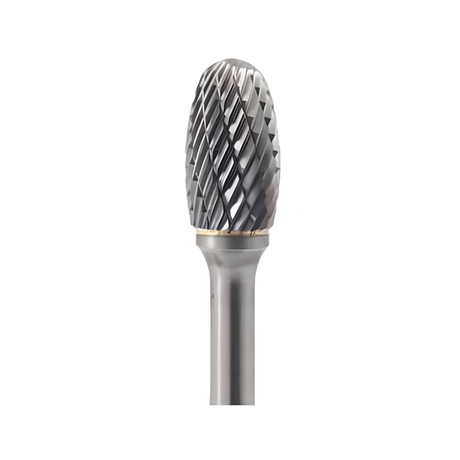
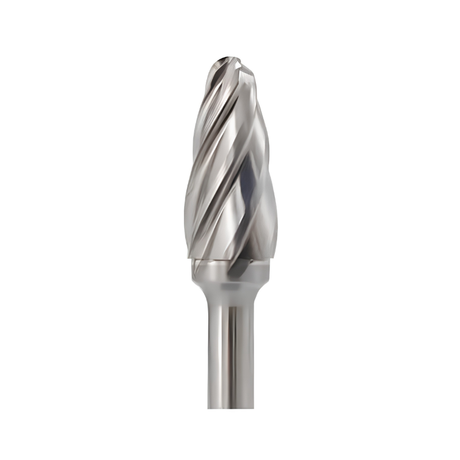
Type F
A tapered head with a rounded tip. Reaches into a corner without leaving a witness mark from a point.
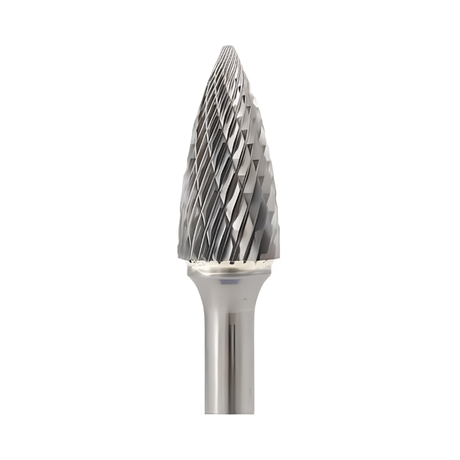
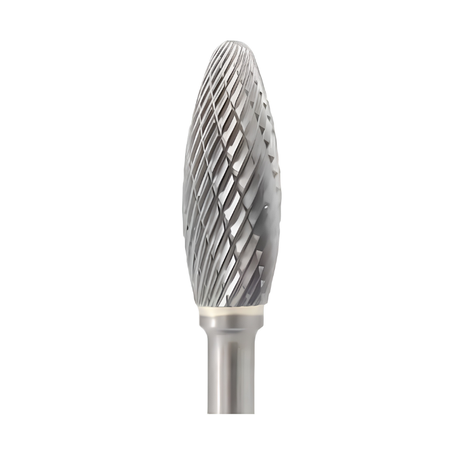

Type J
A cone with a narrower included angle than Type K. Breaks a hole edge without opening the hole out.
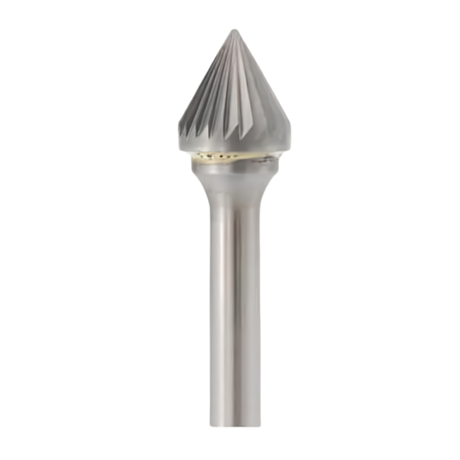
Type K
A 90° included angle, matching the seat of a standard countersunk screw. The hole-entry chamfering burr.
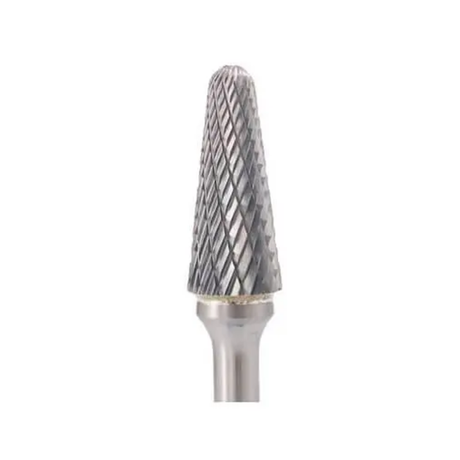
Type L
A tapered cone with a rounded end. Blends a radius where the approach angle is too tight for a cylinder.
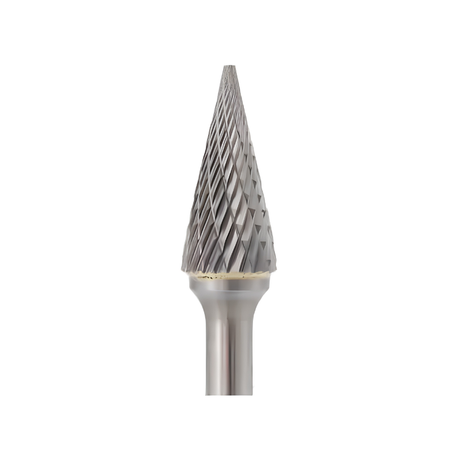
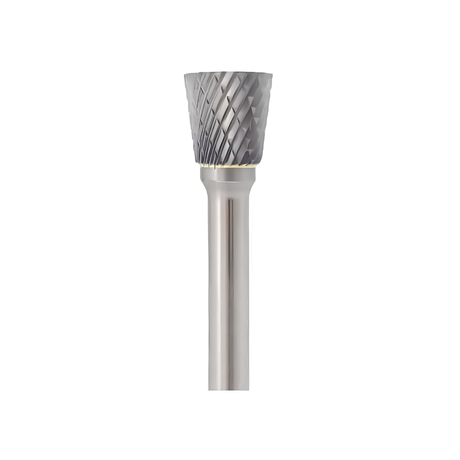
Greyed cut styles are not stocked in that shape. Aluminium cut is made in Types A, B, C, D, F and L only; Types J and K are single cut only.
Shop by the job
If you know the feature rather than the letter, start here. Each job points at the shapes that suit it.
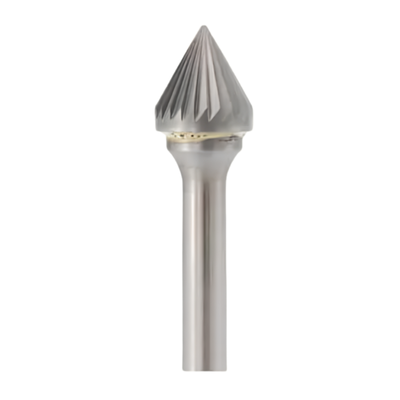
Hole entry chamfers
The burr at a drilled hole entry comes off in one pass with a countersink-form head. Type K matches a countersunk screw seat; Type J is narrower.
Types J, K, M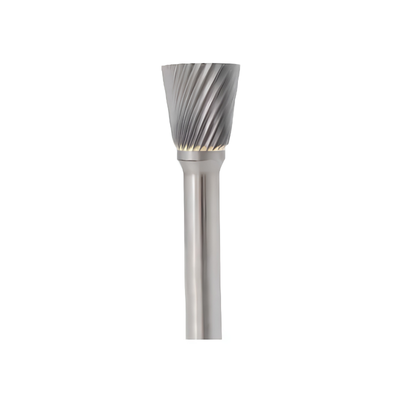
Back faces & cross holes
Passes through the hole and cuts on the way back out, reaching a back-face or cross-hole burr no hand scraper will get to.
Type N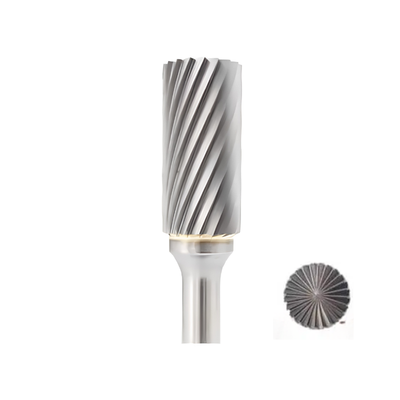
Opening out & truing
Cuts on the flank to straighten a hole or slot wall. Type A will not touch the floor of a pocket; Type B can plunge first.
Types A, B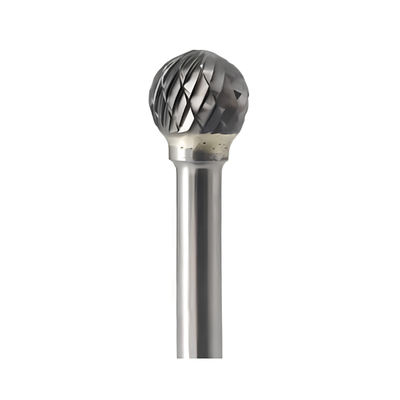
Blending radii
Follows a curve without leaving a facet. A ball for concave radii, an oval for long sweeps, a ball nose cone for tight approach angles.
Types C, D, E, L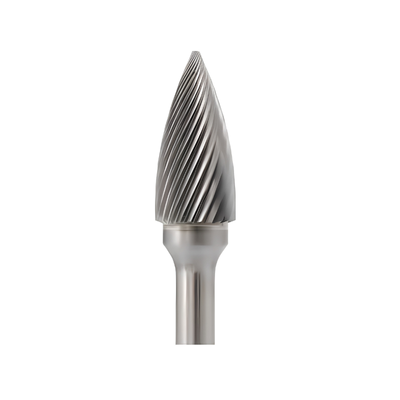
Corners & tight profiles
Puts the cutting edge into a corner without the shank fouling the part. Pointed for sharp corners, ball nose to avoid a witness mark.
Types F, G, H, MShop by what you are cutting
The shape decides where the burr can reach. The cut decides how it behaves in the material — getting this wrong is the usual reason a burr stops cutting or leaves a poor finish.
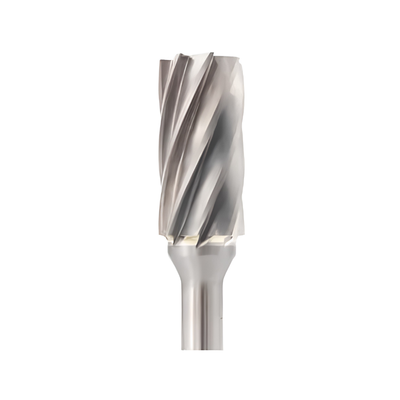
Aluminium & non-ferrous
Soft gummy swarf packs a standard burr within seconds and it stops cutting. Aluminium cut has fewer, deeper, wider-spaced flutes so the chip clears itself.
Brass, copper, bronze, plasticsSteel & stainless
A second flute crossed over the first breaks the chip small, so the tool does not grab in a hand-held grinder and the finish needs no further work.
The default hand-deburring choice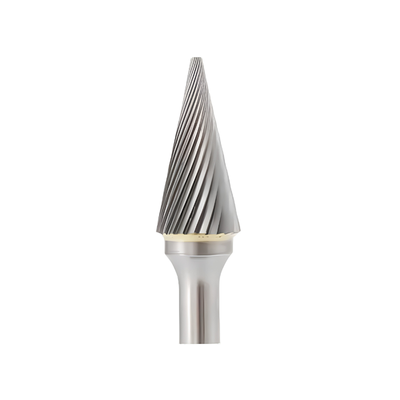
Cast iron & heavy removal
Wider tooth spacing means each tooth takes a heavier bite. Faster stock removal, coarser finish, long chips. Use it where the surface gets worked again.
Weld, flash and casting materialHow to read the range
Every burr in the range is described by three things: the shape letter, the cut style and the head diameter. Get those three right and the part number follows.
| Cut | What it is | Behaviour | Best for |
|---|---|---|---|
| Single cut | One set of helical flutes, widely spaced teeth | Each tooth takes a bigger bite. Fast removal, coarser finish, long stringy chips | Steel, stainless and cast iron where you have material to shift |
| Double cut | A second set of flutes crossed over the first (cross cut or diamond cut) | Smaller chips, less grab, more control by hand, finer finish | The default choice for steel, stainless and most hand-held deburring |
| Aluminium cut | Fewer, deeper, more open gullets | Soft swarf clears itself instead of packing into the flutes | Aluminium, brass, copper, bronze and plastics |
| Shank | Head diameters | Overall length | Typical use |
|---|---|---|---|
| 3mm | 3mm and 4mm | 38mm | Micro deburring, small bores, tight internal corners, pencil grinders |
| 6mm | 6, 8, 10, 12 and 16mm | 50mm to 81mm depending on head length | General shop deburring and stock removal in a standard 6mm die grinder collet |
Head length varies with shape as well as diameter — a 16mm flame has a 36mm head, a 16mm ball has a 14mm head. Every product page lists head diameter, shank diameter, head length and overall length.
Carbide burr FAQs
Which carbide burr should I use on aluminium?
Use an aluminium cut burr. Aluminium, brass, copper and most plastics are soft enough to weld themselves into the flutes of a standard single or double cut burr, and once the gullets pack the tool stops cutting and starts rubbing — you get heat, smearing and a ruined surface rather than swarf. Aluminium cut has fewer, deeper flutes with much wider spacing so the chip clears itself. Protool stocks aluminium cut in Types A, B, C, D, F and L from 6mm to 16mm head diameter. If you need a shape we do not stock in aluminium cut — oval, tree, flame, countersink, cone or inverted cone — single cut is the closer substitute, because its wider tooth spacing clogs less readily than double cut, but expect to clear the flutes more often.
What is the difference between single cut, double cut and aluminium cut?
It is the flute geometry, and it changes how the burr behaves rather than what it is made from — all three are the same tungsten carbide. Single cut has one set of helical flutes with widely spaced teeth, so each tooth takes a heavier bite: material comes off fast, the finish is coarser and the chips come off long and stringy. Double cut adds a second set of flutes crossed over the first, which breaks those chips into small pieces. That makes the tool far less likely to grab in a hand-held grinder, gives you more control and leaves a finer finish, which is why double cut is the usual choice for hand deburring on steel and stainless. Aluminium cut is a specialist form with fewer, deeper and more open gullets, made to stop soft gummy swarf from packing in. Choose single cut for speed, double cut for finish and control, aluminium cut for non-ferrous.
Which carbide burr shape do I need?
Work back from the feature you are cutting. For a hole entry chamfer, use a countersink form — Type K for a 90° included angle, Type J for a narrower one. For a burr on the back face of a hole or a cross-hole intersection, use an inverted cone (Type N), which cuts as you draw it back out. To open out or straighten a hole or slot, use a cylinder: Type A cuts only on the flank, Type B has end teeth and can plunge. To blend a radius or a curved face, use a ball (Type D), oval (Type E), ball nose cylinder (Type C) or ball nose cone (Type L). To reach into a corner or a tight profile, use a pointed tree (Type G), ball nose tree (Type F), flame (Type H) or cone (Type M). Protool stocks all thirteen shapes, Types A through N — there is no Type I in the standard series.
What shank sizes do these carbide burrs come in?
Two: 3mm and 6mm. The 3mm shank carries the 3mm and 4mm heads and is 38mm overall, which suits a pencil grinder or a micro die grinder for small bores and tight internal corners. The 6mm shank carries the 6, 8, 10, 12 and 16mm heads and runs from 50mm to 81mm overall depending on how long the head is. 6mm is the standard collet size on most workshop die grinders in the UK, so it covers the majority of jobs. If your grinder takes 1/4in (6.35mm) collets, a 6mm burr will not run true in it — check the collet size rather than assuming, because the two are close enough to look interchangeable and are not.
How do I deburr the back of a hole or a cross-hole I cannot see?
Use an inverted cone burr (Type N). It is narrow at the shank end and wide at the tip, so you pass it through the hole, tip it against the far face and cut on the withdrawal stroke. That reaches a back-face burr that no hand scraper will get to. The same geometry works for the intersection where a cross hole breaks into a bore, which is one of the hardest burrs to remove in a machined part — the flat top face of the cone lets you clean the intersection square rather than rolling the edge over into the bore. Protool stocks Type N in single and double cut, 3mm to 16mm head. For access through a small hole, a 3mm head on a 3mm shank will pass through a hole a 6mm head will not.
Can I use a carbide burr in a drill instead of a die grinder?
You can, but it will not work well and it wears the tool quickly. Carbide burrs are designed to run at die grinder speeds — tens of thousands of rpm — where the cutting edge shears the material cleanly. A mains or cordless drill tops out an order of magnitude lower, so the teeth rub and chip instead of cutting, the burr loads up, and you push harder to compensate, which is how burrs get snapped. A drill chuck also holds a 6mm shank far less concentrically than a collet, so the head runs out and chatters. If a drill is genuinely all you have, take very light passes, keep the burr moving and expect a short tool life. For occasional hand deburring on drilled holes, a hand deburring tool or a countersink is the better answer.
Do you sell carbide burr sets?
No — Vortex carbide burrs are stocked and sold individually, not in boxed sets. In practice that works out better for a working shop: sets are priced around a spread of shapes you may never touch, and when you wear out the one shape you actually use you are buying the whole set again. Buying singles means you can stock two or three of the shape and cut you use every week and replace exactly that. If you want a starting spread for a general workshop, a 6mm double cut ball (Type D), a 6mm double cut cylinder with end cut (Type B) and a 10mm single cut 90° countersink (Type K) will cover most day-to-day deburring. All items are held in UK stock.
Not sure which burr fits the job?
Our technical team works with aerospace, motorsport and precision engineering shops every day. Tell us the feature you are trying to deburr and we will tell you what we would reach for.
